How Food Packaging Machines Are Built, Not Just Sold.
From a confirmed drawing to a tested machine: how TOP Y Machinery, a food packaging machine manufacturer in Foshan, moves every order through drawing, batch assembly, whole-unit commissioning and real-material testing, and what changes on a non-standard build.
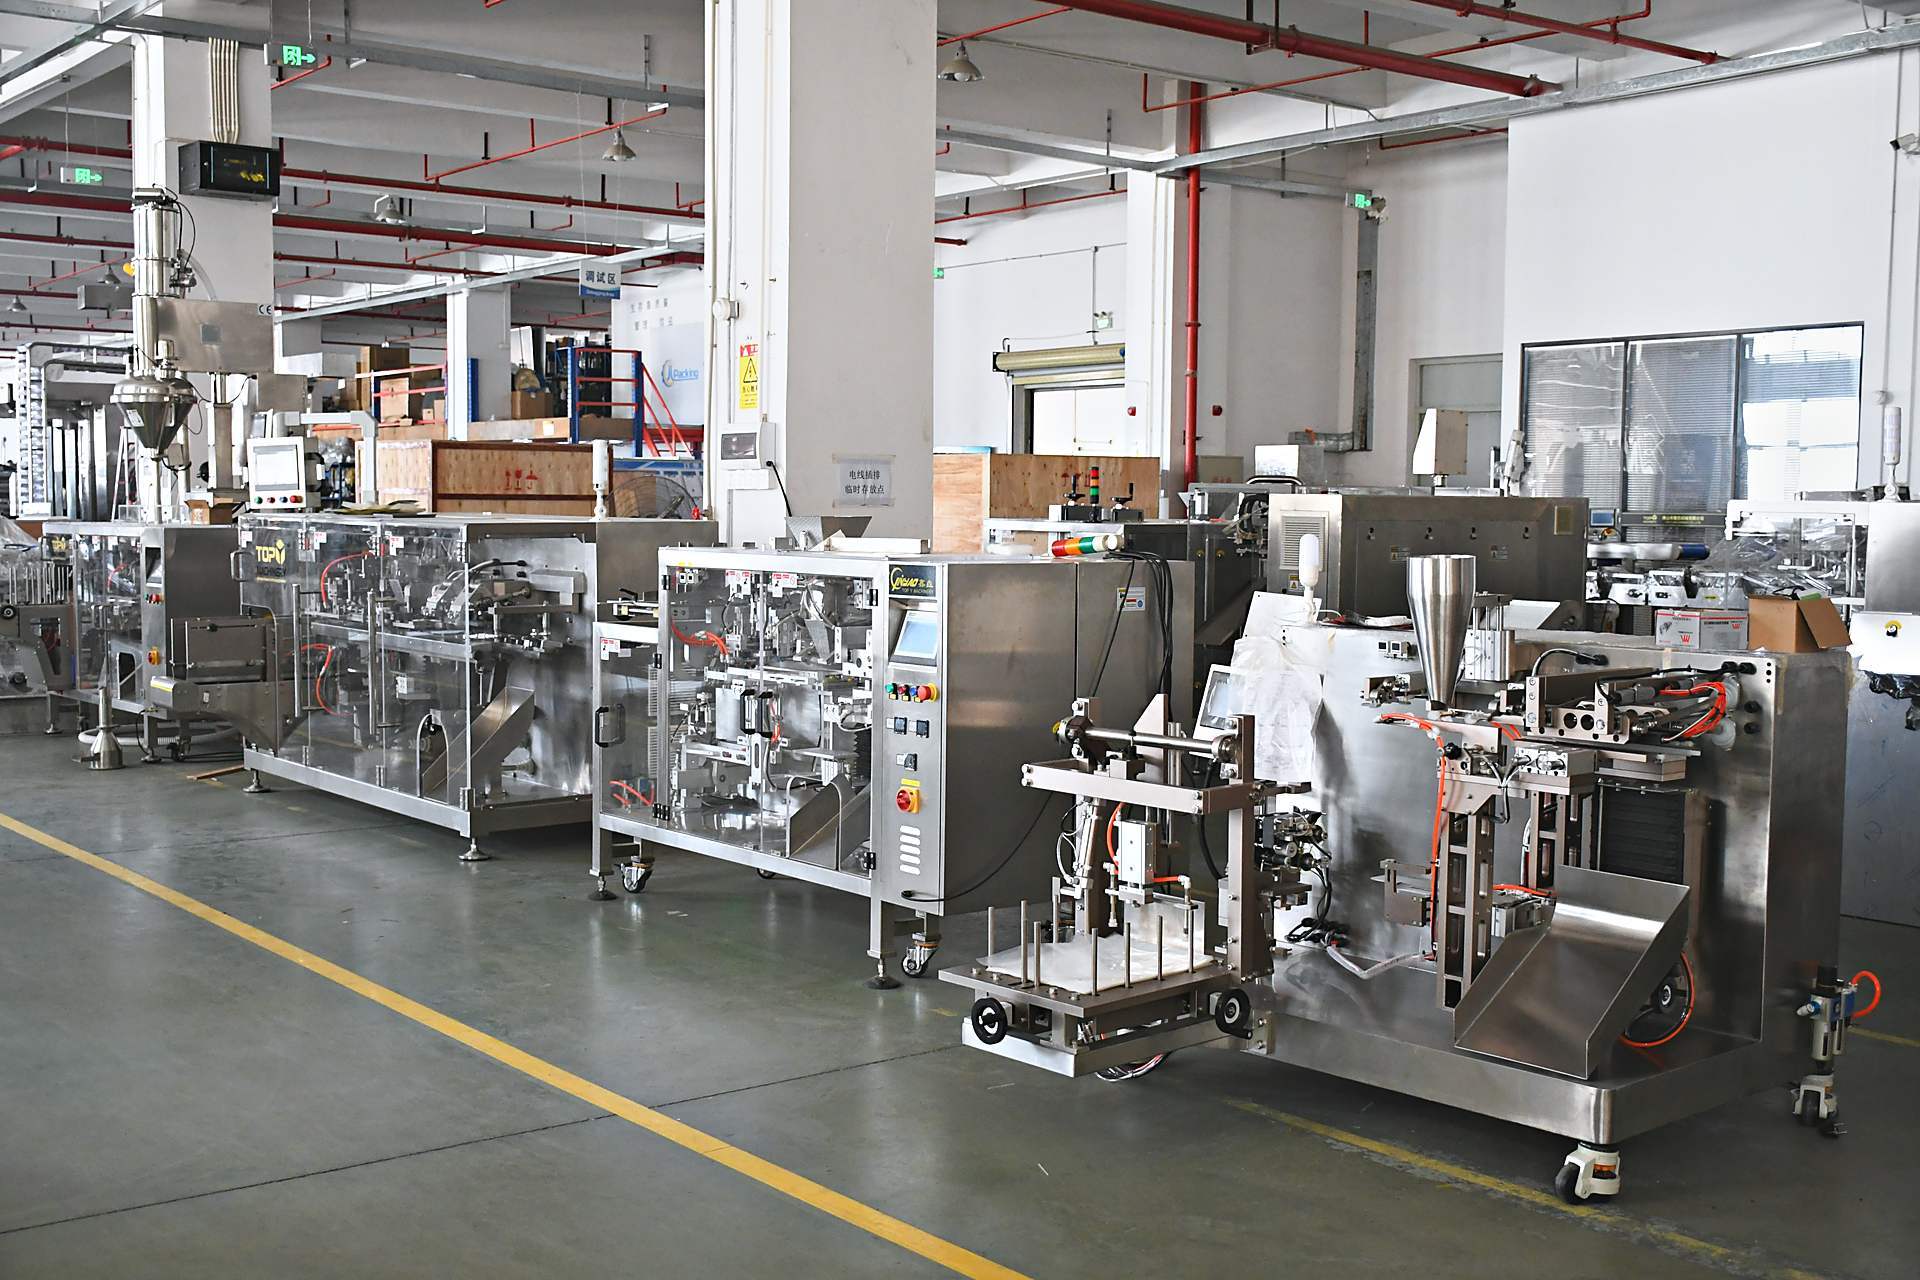
Food packaging machine factory in Foshan, Guangdong, China.
Integrated under one roof, rather than assembled from suppliers.
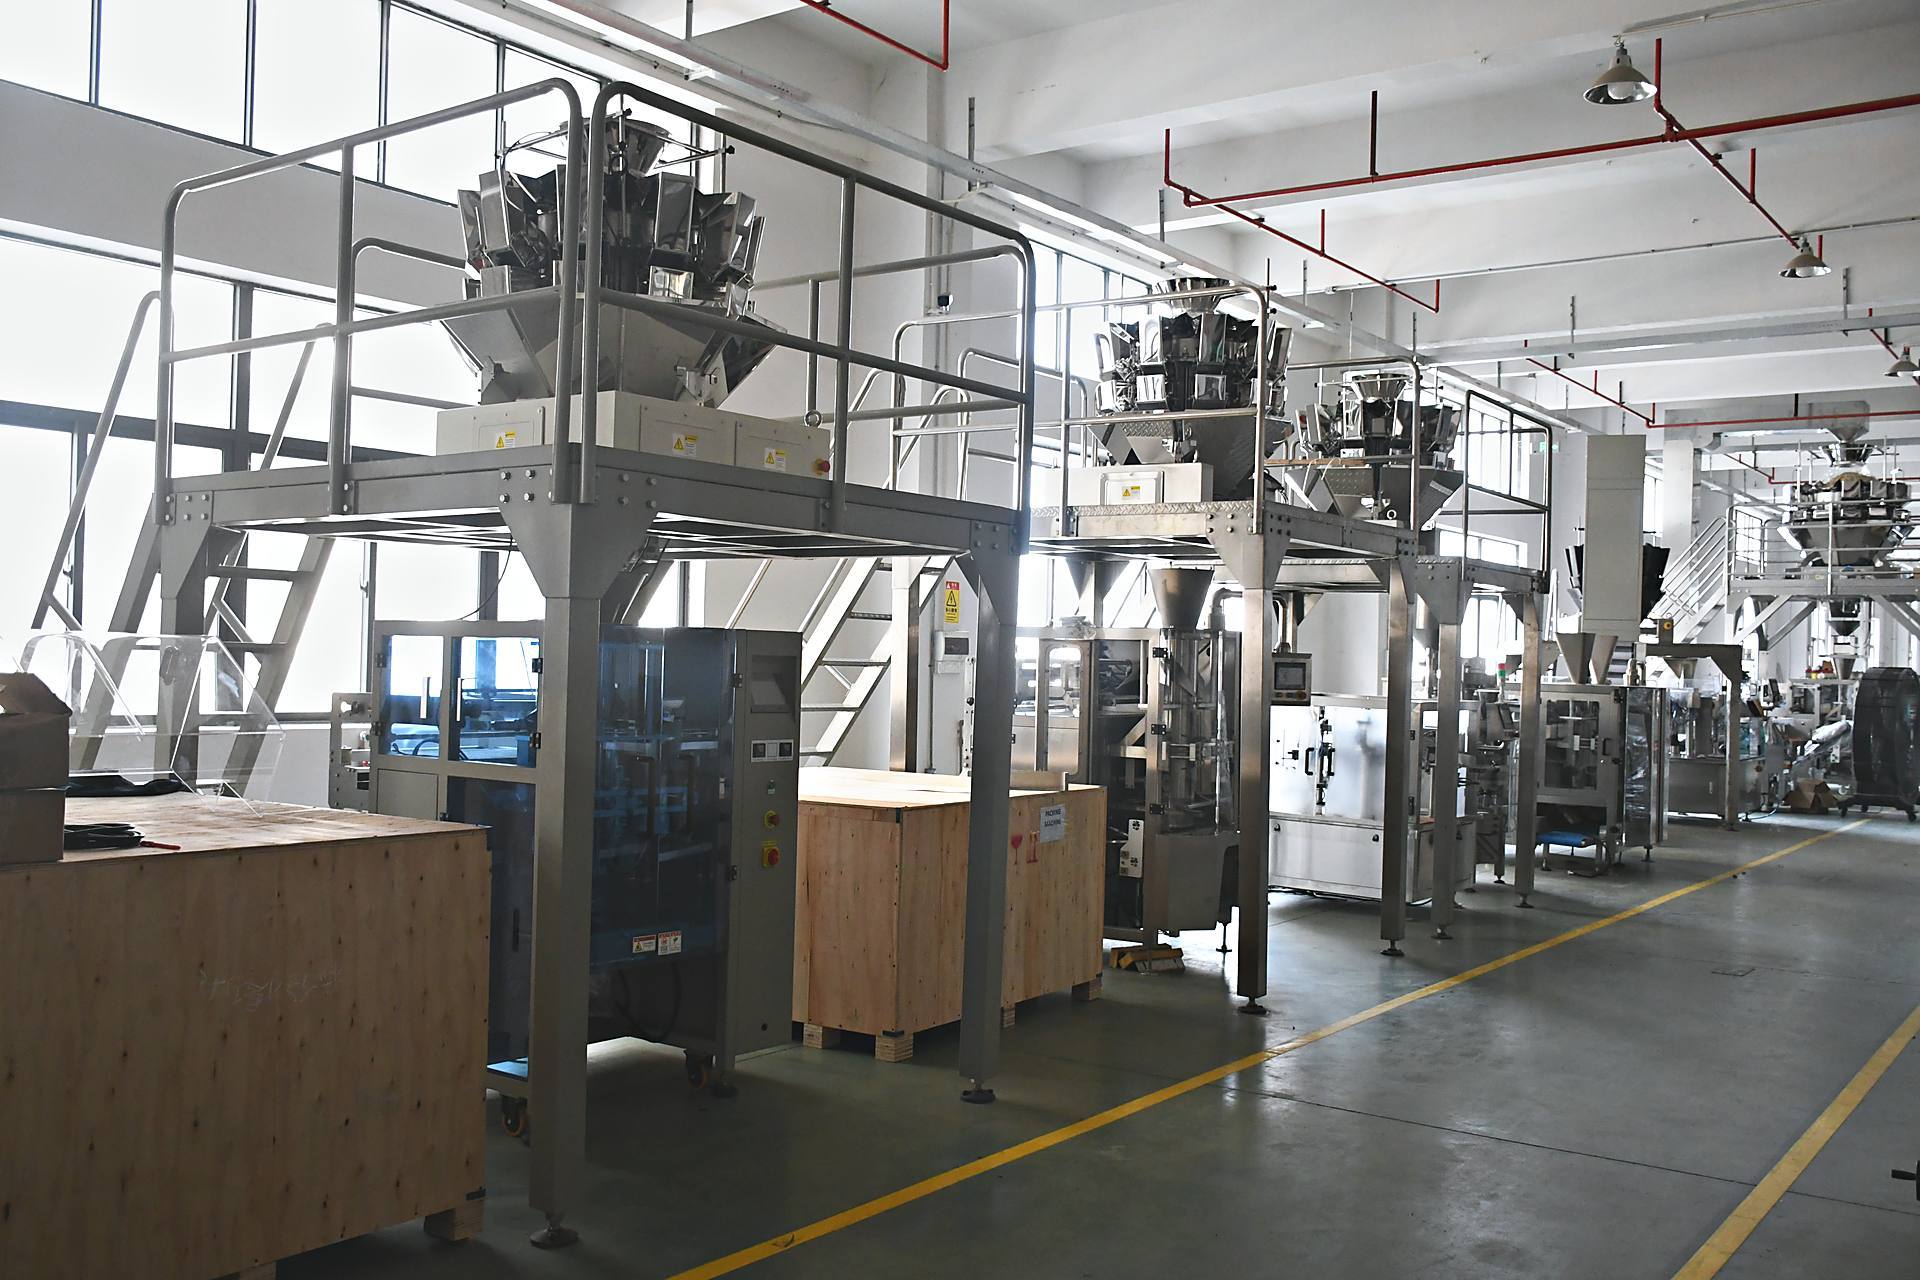
Built in batches, then commissioned as one complete machine.
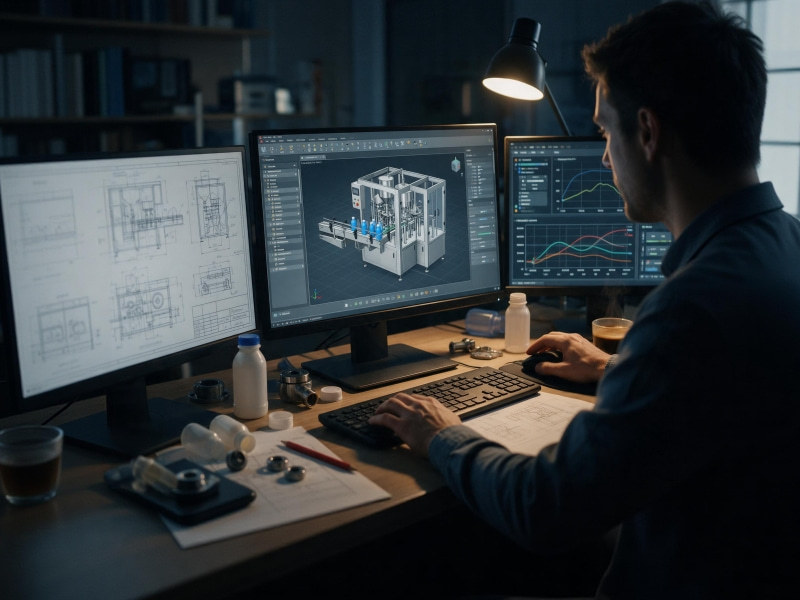
Machine dimensions and production operations marked on the drawing.
Custom machines and complete automatic packaging lines.
One Foshan site. Design, manufacture and build, together.
As a food packaging machine manufacturer, TOP Y Machinery runs design, manufacturing and shipment from one Foshan base. No split between companies: a change on the drawing reaches the shop floor directly.
| Manufacturing fact | Detail |
|---|---|
| Manufacturing base | Foshan, Guangdong, China, at a single production site. |
| Established | October 2011. |
| Business model | Design, manufacture and sales integrated in one company. |
| Manufacturing scope | Custom food packaging machines and non-standard automatic packaging lines, including pre-made pouch machines and roll-film form-fill-seal machines. |
| Production organisation | Drawing-led build: dimensions and production operations marked on the drawing, assembly carried out in batches, complete machine commissioned as a whole unit. |
| Workshop floor area | 4,500+ m² at a single production site. |
| Engineering and production team | Over 50 workers, including electrical engineers, mechanical design engineers, commissioning engineers and after-sales engineers, plus purchasing, production and quality managers. |
| Monthly build capacity | Close to 70 sets custom food packaging machines per month. |
| Typical lead time, standard and custom | Prototypes 7–20 days; standard machines 30 days; non-standard builds 40–60 days; highly complex machines or complete lines 60–90 days. |
Every machine starts as a marked-up drawing.
Production begins on paper. Dimensions and operations are marked onto the drawing itself, so the shop floor builds to a document, not an interpretation.
Three things the drawing settles before anything is built
- Dimensions. The machine's overall size and the space each unit occupies are fixed on the drawing, not decided on the floor.
- Operations. The production operations are marked in detail, so the machine is built in a defined order rather than in whatever order is convenient.
- Confirmation. The technical drawings for the order are issued for the customer's review and confirmation before production begins.
This is also the honest answer to "when will my machine be ready?"
For a custom machine the schedule only becomes real once the drawing is confirmed. Before that point no manufacturer can commit to a date with any confidence, which is why drawing confirmation is the gate that starts the production clock, not the purchase order.
Built in batches first, then commissioned as one machine.
Each batch is proven on its own before the next one starts. The complete machine is then assembled and run as a single unit.
Every sub-assembly that was verified in batches now has to behave together: feeding, metering, bag forming, sealing, drive and control running as a single machine.
Faults surface inside a batch
A problem in one sub-assembly shows up while that batch is being proven, not at final testing, when correcting it means taking the machine apart again.
Sub-assemblies proven before integration
Each batch is verified on its own, so integration is a test of how the parts work together, not a first attempt at making any of them work.
Handed over as one unit
The customer receives a machine that has already run as a whole line, rather than a set of units whose combined behaviour is unknown until installation.
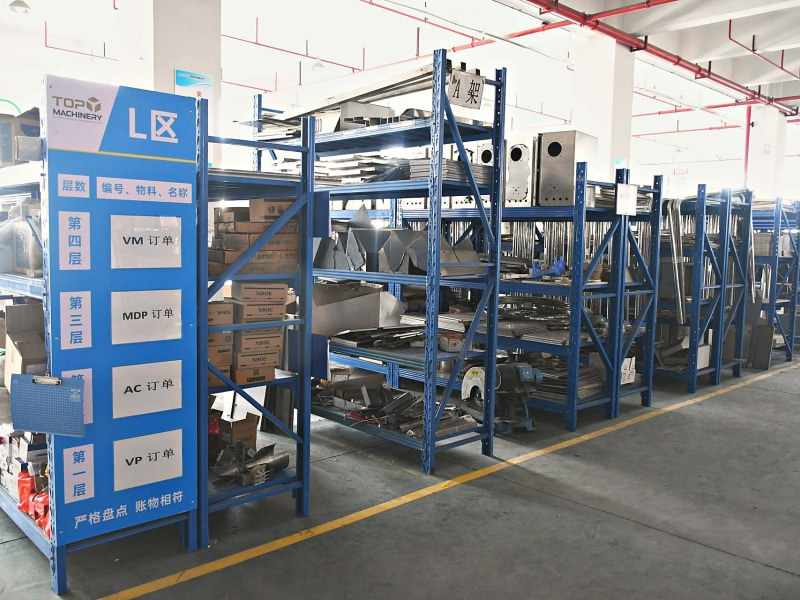
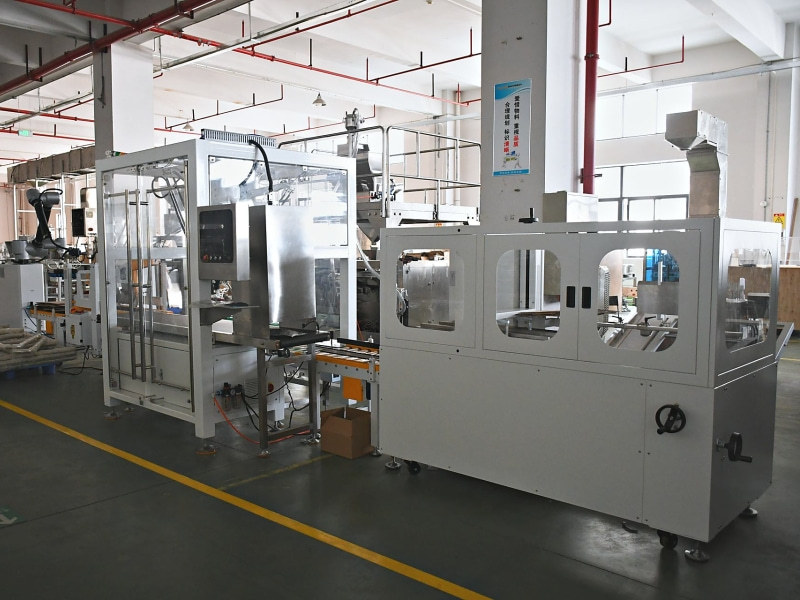
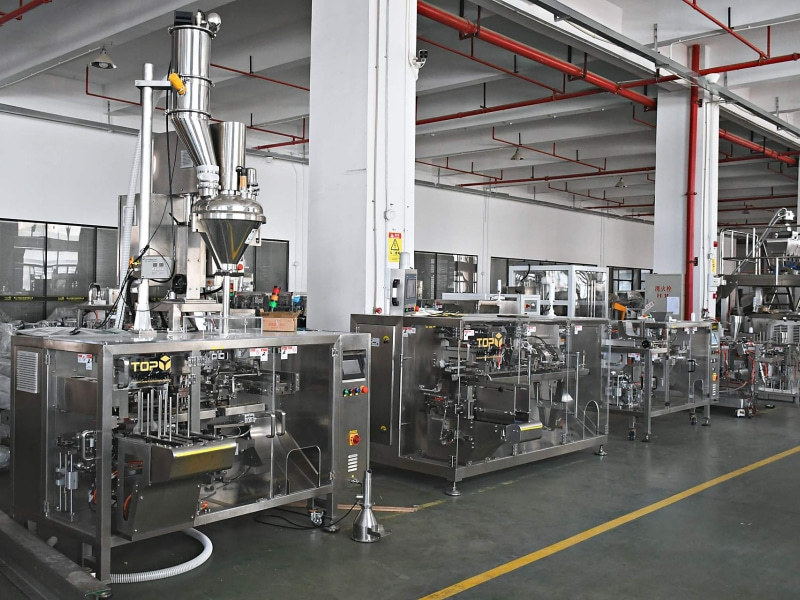
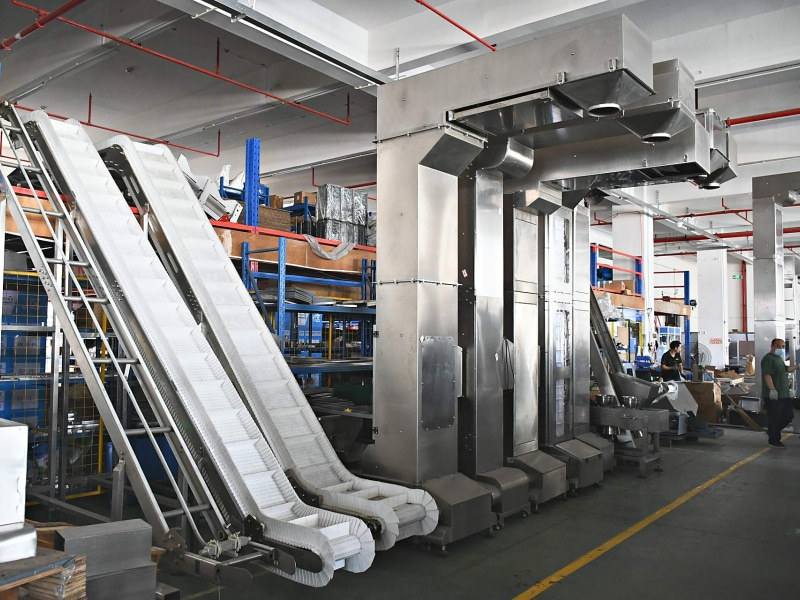
Where drawings become machines.
The food packaging machine factory floor, where TOP Y's machines are assembled, commissioned and prepared for shipment.
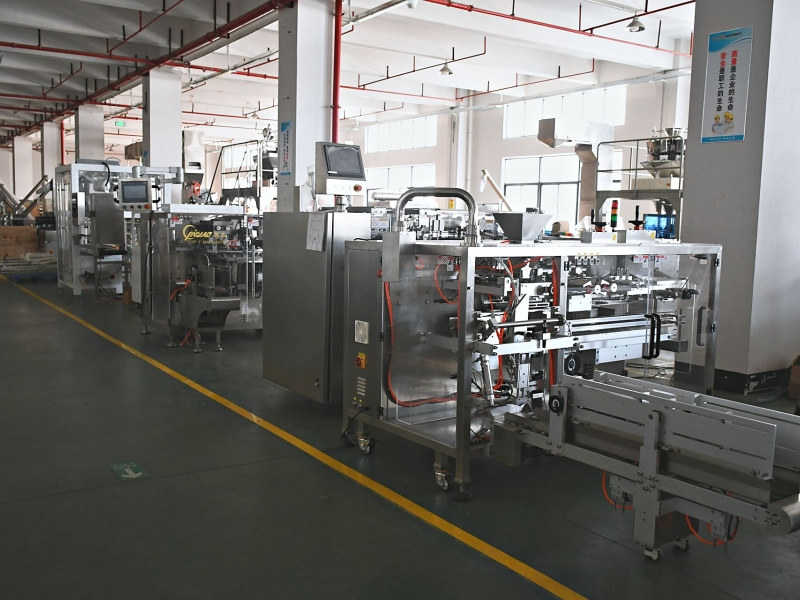
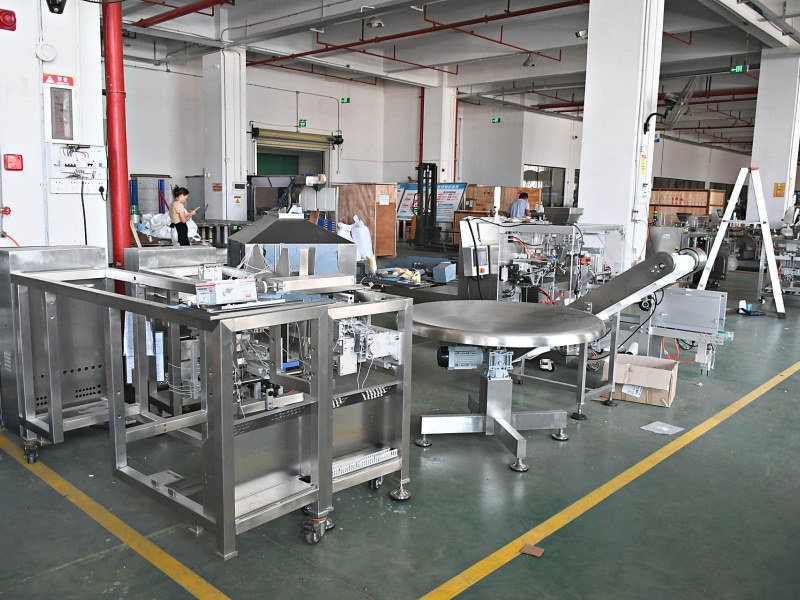
From a confirmed drawing to a crated machine: nine stages.
What happens to an order between drawing sign-off and dispatch. Each stage has a control point, where a defect can still be caught cheaply.
Technical drawing confirmed
The order's technical drawings are issued for customer review and confirmation. Nothing is cut before this gate is passed.
ControlDrawing confirmation, the gate that starts the production clock.Production scheduled
Working hours for each department are scheduled backwards from the delivery date of the individual order, with separate handling for urgent orders.
ControlSchedule set per order, not per product category.Parts and fabricated items prepared
Standard components are drawn from stock; non-standard items are made or sourced to the confirmed drawing before they reach the assembly area.
ControlNon-standard items checked against the drawing, not against a sample.Batch assembly
The machine is assembled in batches, and each batch is made to run correctly before the build moves to the next one.
ControlEach batch proven before the next begins.Electrical assembly and control
Circuit diagrams and control programming are produced alongside the mechanical design, so wiring and logic are built for the machine rather than retro-fitted to it.
ControlMechanical and electrical drawings reviewed together per order.Whole-unit commissioning
The verified batches are integrated and the complete machine is assembled and run as one unit, with feeding, metering, bag forming, sealing, drive and control behaving together.
ControlWhole-machine run, not a per-unit check.Real-material test run
Customers send their own packaging material for testing on the actual machine, and receive the test video and report. This is the point at which the machine meets the real product instead of a specification.
ControlTested on the customer's own material.Pre-shipment inspection
Inspection footage, photographs and the formal report are produced before the machine is released for shipment.
ControlDocumented release, the machine does not ship on a verbal approval.Export packing and dispatch
The machine is packed in moisture-proof wooden crating and dispatched as FCL or LCL, with the customs documentation prepared for the destination.
ControlProtection and documentation matched to the shipping mode.What a non-standard order actually changes in the factory.
A non-standard machine has no previous unit to copy from. The drawing work, parts, assembly and verification method all shift.
| What changes | What happens in the factory |
|---|---|
| Drawing workload | A standard machine is built to already-reviewed standard drawings. A non-standard order requires the non-standard solution to be designed and drawn first, which is why the drawing stage, not the assembly stage, is where a custom project is won or lost. |
| Parts and fabricated items | Standard components are called from stock. Items specific to the order are made or sourced to the confirmed drawing, then checked into assembly against that drawing. |
| Assembly organisation | The batch division and any order-specific tooling have to be planned per machine, because the structure and dimensions differ from the standard build. |
| Verification method | A standard machine follows a known verification route. On a custom build the real-material test run carries more weight, because it is the first time this particular configuration meets an actual product. |
| Lead time | Determined by drawing confirmation plus manufacturing time, and therefore quoted per project rather than from a fixed table. Typical range: prototypes 7–20 days, standard machines 30 days, non-standard builds 40–60 days, and 60–90 days for the most complex machines or complete lines. |
Which packaging formats, sealing methods, feeding systems, automation levels and workshop-fit layouts TOP Y can configure is covered in detail on the Custom Packaging Machinery page. This page deliberately stays on the production side: what those choices cost you in drawing work, assembly planning and verification.
Come and see the workshop.
Send us your product, pouch format and workshop dimensions, and we will show how a food packaging machine manufacturer draws, builds and tests your line.